KARTIKEYFASTENERS
Plant & machinery

Four units.
73 machines.

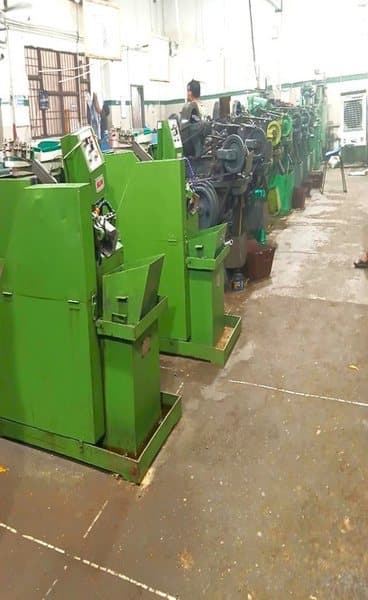
Plot No. 43, 44, 166 & 299 — Phase 9, SAS Nagar, Mohali, Punjab. Forming, threading, slotting, heat treatment, plating and sorting all sit inside our own walls — which is why a schedule change on Monday does not become a subcontractor's problem on Thursday.

0
Header machines
0
Rolling machines
0
Slotters
0
Furnaces & barrels
0
Classes of test gear
On the floor

The works at Phase 9

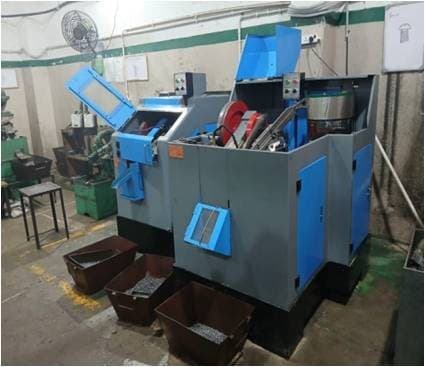
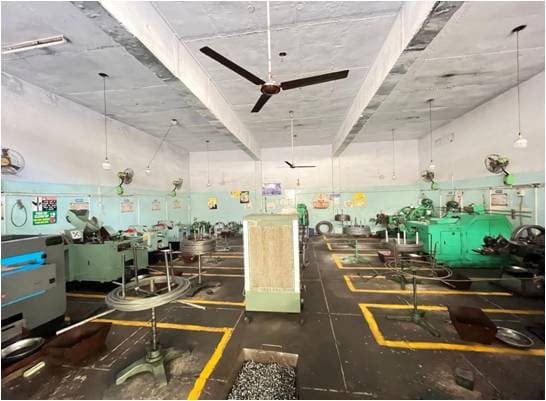
Header machine shop floorHeader machine shop floor
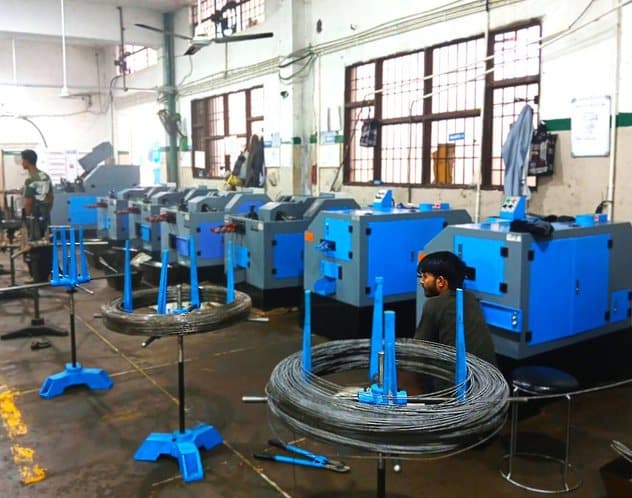
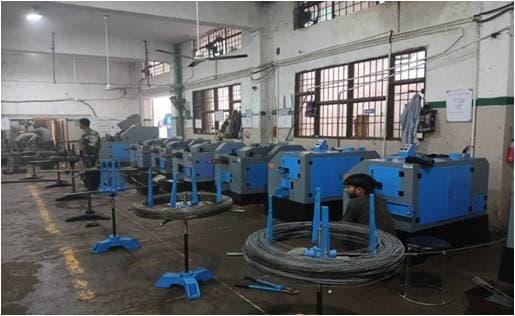
Bank of header machines with wire standsBank of header machines with wire stands
Thread rolling lineThread rolling line
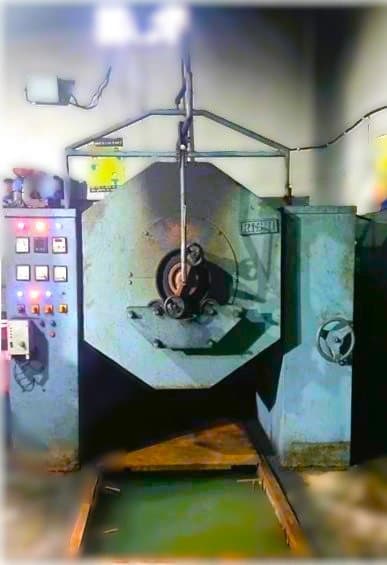
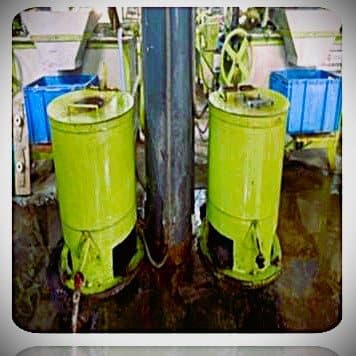
Plating and heat treatment plantPlating and heat treatment plant
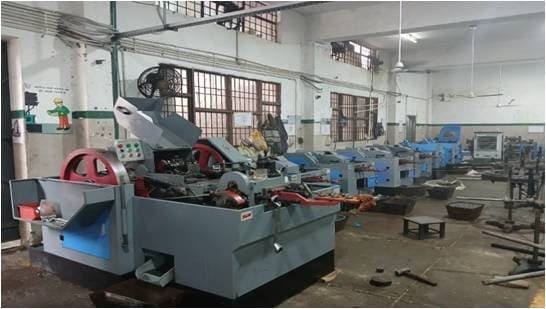
Row of forming machinesRow of forming machines
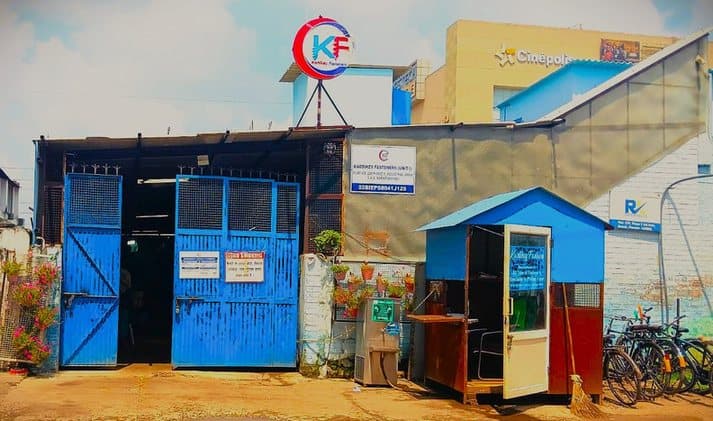
Kartikey Fasteners unit entranceKartikey Fasteners unit entrance
Manufacturing process

Wire in. Packed carton out.

Seven stages, each with its own critical-to-quality checks recorded on a PQC sheet before the batch moves on.

Raw Material — Kartikey Fasteners01

Raw Material

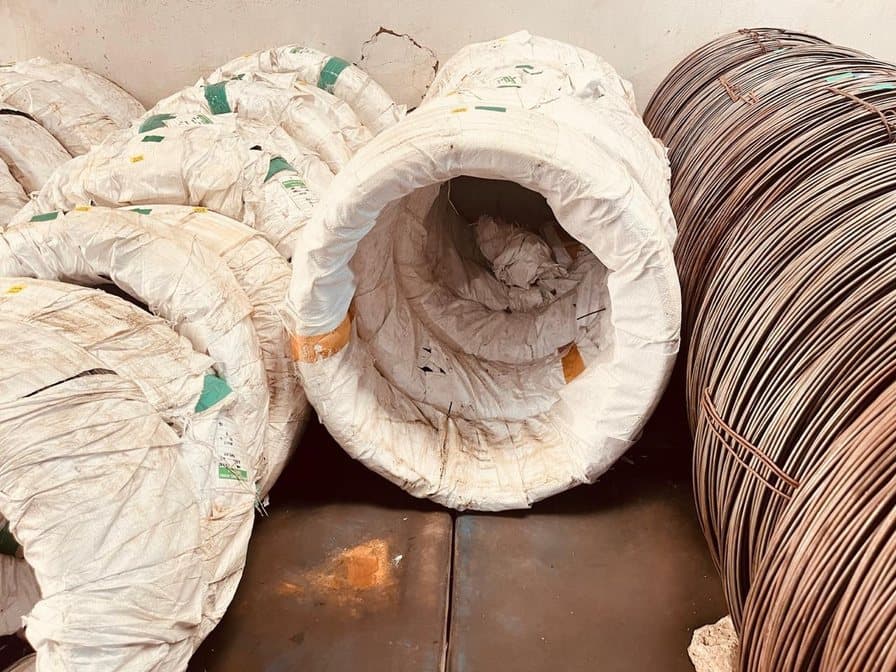
MS and SS wire is drawn in from vetted vendors across a full range of diameters. Every invoice arrives with a mill test certificate stating chemical composition and mechanical properties, and wire pieces go out for independent third-party testing.

  • MTC received with every consignment
  • Wire diameter verified on vernier caliper
  • Third-party wire testing with MTC report
Heading — Kartikey Fasteners02

Heading

Wire is cold headed on our own header machines. Tooling is selected per part — the right punch and the right die — and the first-off is dimensioned before the run is released.

  • Blank dia, head dia & washer dia
  • Length, head thickness & washer thickness
  • Micrometer, vernier caliper and bit check
Rolling — Kartikey Fasteners03

Rolling

Threads are formed — not cut — by rolling the blank between dies, deforming the stock so the grain follows the thread profile. Rolling tooling is prepared per screw.

  • Thread diameter and length
  • Go / No-Go ring gauge on machine screws
  • Visual point and thread check, PQC sheet filled
Heat Treatment — Kartikey Fasteners04

Heat Treatment

Where the part or the customer calls for it, material moves to the plating section for hardening and tempering, then is cleaned by acidification or casting cleaning before finishing.

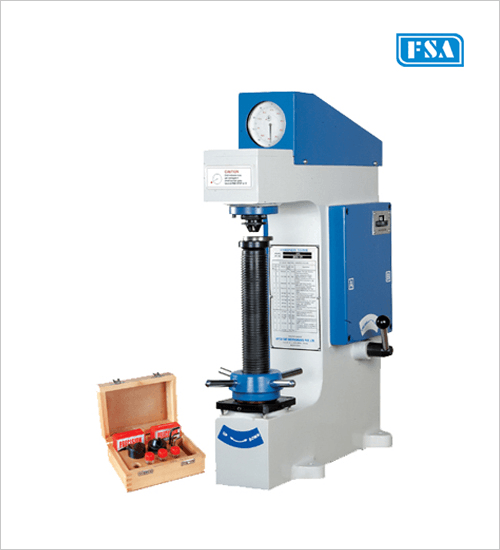
  • Hardness verified on Rockwell hardness tester
  • Rotary furnace and tempering to lot
  • Acidification / casting clean before plating
Plating — Kartikey Fasteners05

Plating

Barrel plating in zinc, tin, copper or nickel to the specified finish, followed by the dip process — plain zinc or RoHS — and drying.

  • Zinc, tin, copper and nickel barrels
  • Plain zinc and RoHS dip process
  • Thread ring gauge Go / No-Go after plating
Segregation — Kartikey Fasteners06

Segregation

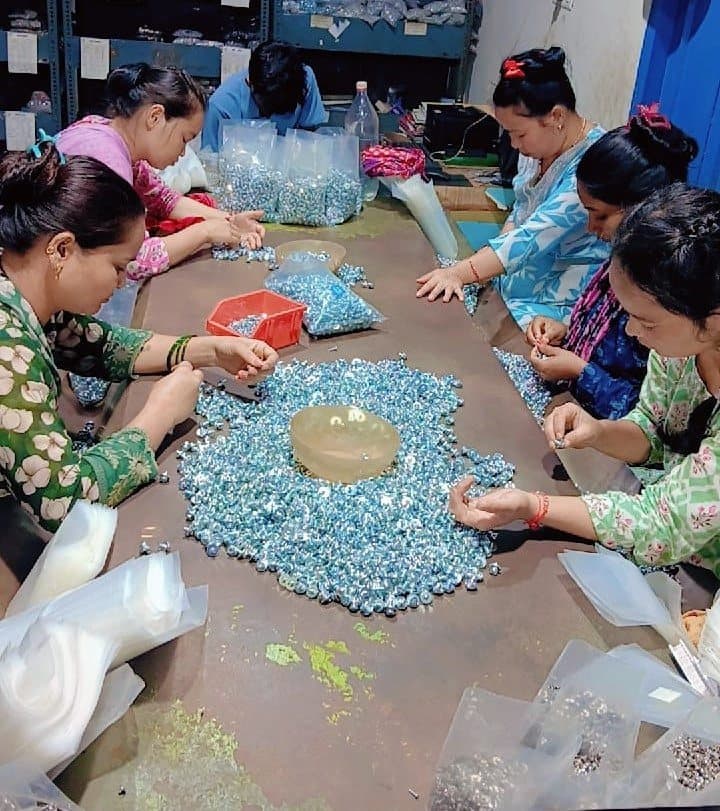
Every plated lot passes through the sorting section, where final quality is judged piece by piece and anything out of spec is pulled from the batch.

  • Damaged thread and burr on thread
  • Head out and broken screws
  • Improper plating
Packing — Kartikey Fasteners07

Packing

Sorted product is counted, bagged and labelled by size, then packed into branded sacks and cartons ready for dispatch.

  • Labelled bags identified by size
  • Branded sacks for bulk quantities
  • Cartons palletised for dispatch
Master list

Machinery, unit by unit

73 machines across 4 plots in Phase 9, SAS Nagar.

Plot 43

Bolt forming
MachineryMakeCapacity / machineQty
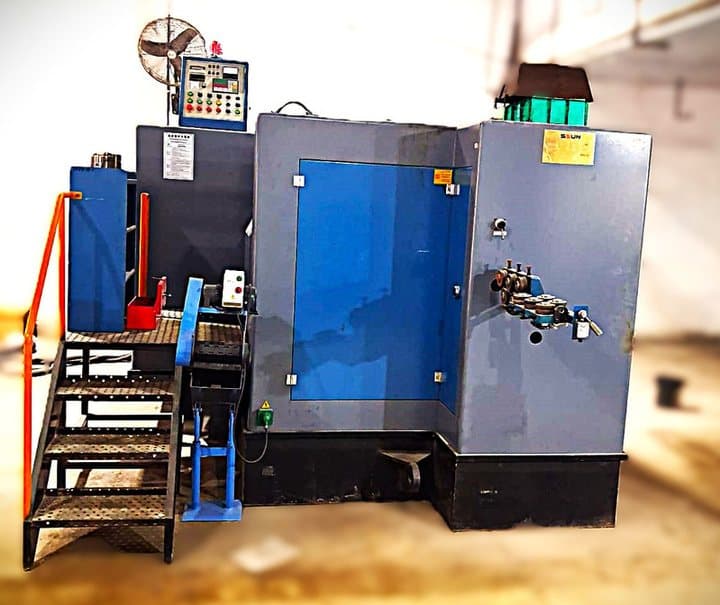
Bolt FormerSUN1000 kg1

Plot 44

Heading, rolling, slotting & washer assembly
MachineryMakeCapacity / machineQty
Header MachineSUN60 kg3
Header MachineLocal120 kg4
Header MachineTop Stability Machine Industry Co. Ltd.150 kg1
Rolling MachineSUN150 kg2
Rolling MachineSUN-J150 kg1
Rolling MachineChien Tsai Machinery Co. Ltd.150 kg1
Rolling MachineLocal100 kg11
Washer AssemblySUN100 kg2
SlotterSUN120 kg2
SlotterLocal80 kg9

Plot 166

Heading
MachineryMakeCapacity / machineQty
Header MachineSUN120 kg6
Header MachineSUN50 kg2
Header MachineGwo Ling Machinery Company50 kg2
Header MachineLocal100 kg12

Plot 299

Heat treatment & plating
MachineryMakeCapacity / machineQty
Rotary FurnaceLocal120 kg / lot2
Tempering MachineLocal60 kg / lot1
Zinc BarrelLocal50 kg / lot3
Zinc BarrelLocal30 kg / lot4
500 Hrs Plating BarrelLocal30 kg / lot2
Nickel BarrelLocal30 kg / lot2
Measurement

Calibrated instruments, not opinions

Dimensions, hardness, torque, depth and finish are each measured on dedicated, calibrated gear. The list below is the equipment register we work to.

Rockwell hardness
Rockwell hardness
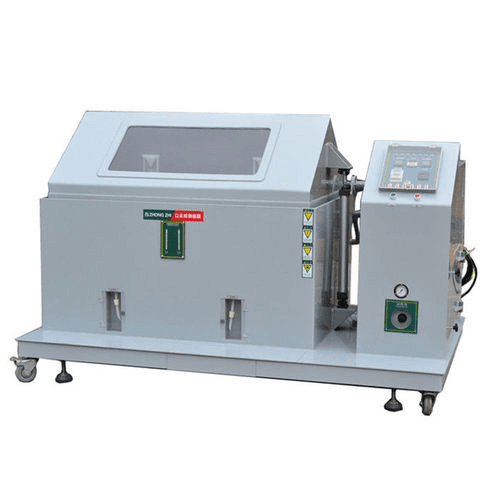
Salt spray chamber
Salt spray chamber
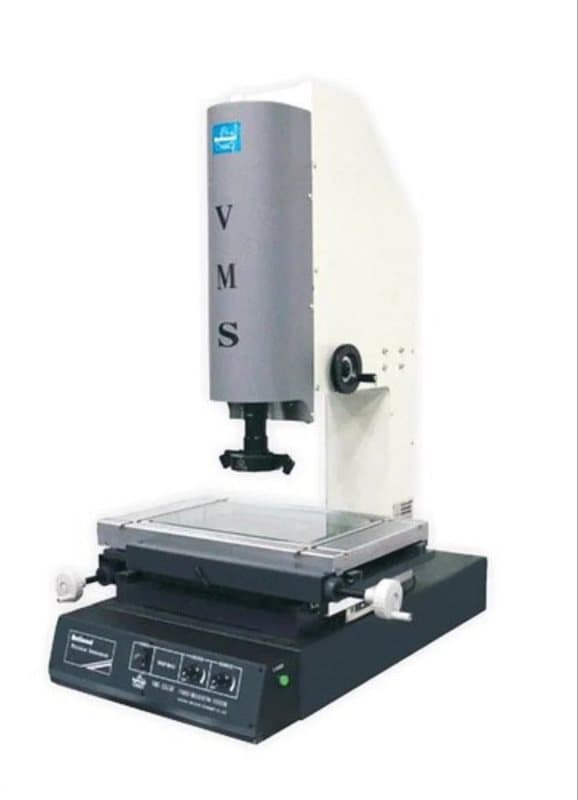
Vision measuring
Vision measuring
Test equipmentMakeLeast countRangeUsed for
MicrometerBaker / Insize0.01 mm0 – 25 mmDimension
Digital MicrometerBaker0.01 mm0 – 25 mmDimension
Digital Vernier CaliperInsize0.01 mm0 – 150 mmDimension
Digital Depth GaugeInsize0.001 mm0 – 300 mmDepth
Thread Ring GaugeBakerAll sizesThread & tolerances
Rockwell Hardness TesterMETAHRCHardness test
Grinding MachineCarburization test
Hammer0.5 kgHead soundness test
Torque WrenchDrebon1 – 12 NmTorsion test
Torque TesterInsize1 – 6 NmTorque test
Digital Weighing MachineSamson0.5 kg0 – 300 kgTorsion test
Vision Measuring MachineQualitechDimension
Salt Spray Test ChamberQualitechFinish (SST)

Heading CTQ

Blank dia, head dia, washer dia, length, washer thickness and head thickness — plus a bit check.

Rolling CTQ

Thread dia and length on micrometer and vernier, Go / No-Go gauge on machine screws, visual point and thread check.

Post-plating

Thread ring gauge Go / No-Go after the dip and dry, then piece-by-piece segregation.

Come and see it in person.

We like our customers on the floor. 09:00 – 17:30, Monday – Saturday.